If you’ve ever stood in front of a Wire Cut EDM machine, watching a thin brass thread zip through a workpiece with nanometer-precision cuts, you know it’s equal parts art and engineering. As someone who’s spent the last decade running a Wire Cut EDM supply business—helping shops, prototyping labs, and job shops get their machines tuned correctly—I can’t tell you how many times I’ve heard, “My cuts are too rough,” or “The thread keeps breaking mid-job.” Nine times out of ten, the culprit isn’t a faulty machine or bad wire; it’s misadjusted pulse parameters. Wire Cut EDM
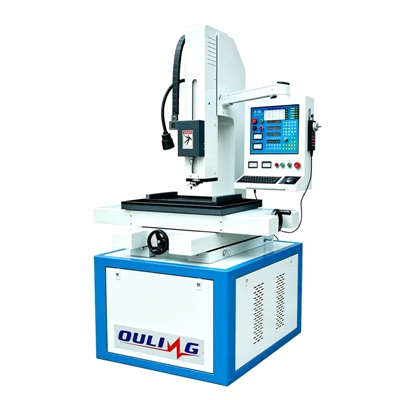
Pulse parameters are the core of how Wire Cut EDM works, really. The process erodes material by creating tiny, controlled electrical sparks between the wire and the workpiece, submerged in a dielectric fluid (usually deionized water). Each spark is triggered by a pulse of electricity, so getting that pulse’s on-time, off-time, voltage, and amperage right is non-negotiable. Mess those up, and you’re either wasting material, snapping wire, or ending up with a part that doesn’t meet print specs. Let me walk you through how to adjust these parameters like someone who’s fixed these exact problems dozens of times, not some textbook writer who’s never turned a wrench on a CNC machine.
First, let’s get clear on the key pulse terms, because if you mix these up, you’ll make every wrong adjustment possible. Pulse On-Time (often labeled as Ton) is exactly that: how long the spark is active, in microseconds (µs), for each cycle. Pulse Off-Time (Toff) is how long there’s a gap between sparks, giving the dielectric fluid time to flush away the eroded material (called “debris”) and cool the area. Then there’s Peak Current (Ip) — the intensity of each spark, measured in amps — and Servo Reference Voltage (or Gap Voltage), which controls how far the wire is from the workpiece at any given moment, ensuring sparks happen consistently without shorting out.
I’ll start with Pulse On-Time, because that’s the parameter I get asked about most. Most shops default to a generic Ton setting, like 15 µs, no matter the material or cut thickness. That’s a rookie mistake. Here’s the rule I’ve honed over years: for thin workpieces (under 10mm, like small brackets or electronic connectors), you want a shorter Ton, usually 10–15 µs. Shorter sparks mean smaller, more precise craters on the workpiece, so you get a smoother surface finish. But if you’re cutting thick material (over 25mm, like mold bases or large tool steel blocks), you need a longer Ton—20–30 µs. A longer spark has more time to erode deep into the material, which keeps the cut rate (how fast the wire travels through the workpiece) from dropping to a crawl. I learned this the hard way: a customer once was cutting a 30mm die block and kept their Ton at 12 µs, and their cut speed was half what it should be. Switching to 25 µs boosted their speed by 70% without hurting precision. The catch? If Ton is too long for the material thickness, you’ll get bigger craters, rougher surfaces, and more wire breaks because the debris doesn’t get flushed out fast enough.
Next up is Pulse Off-Time, the unsung hero of Wire Cut EDM. A lot of guys skip over Toff, assuming the machine’s default is fine, but that’s a huge mistake. Toff is all about debris evacuation. If Ton is how hard each spark hits, Toff is how much time you give the dielectric fluid to wash that spent material away. For thin workpieces, you need a shorter Toff—usually 4–10 µs—because there’s less debris to flush out, and faster cuts mean faster cycles. But for thick workpieces, you need a longer Toff, like 15–25 µs. I had a customer cutting a 40mm titanium aerospace bracket who kept getting “short circuits” every few minutes, snapping their 0.2mm wire twice a day. They had their Toff set at 8 µs, way too short for the thick titanium’s fine, dense debris. Cranking Toff to 20 µs fixed the short circuits, cut their wire break rate to almost zero, and even improved surface finish because there was no leftover debris causing stray sparks. A quick rule of thumb here: if you’re seeing frequent wire breaks or rough, pitted surfaces, add 5–10 µs to your Toff. If your machine’s alarm is warning of debris buildup, that’s your Toff telling you it’s not enough.
Peak Current is another make-or-break parameter, and it’s tied directly to both cut speed and surface quality. Higher Ip means more powerful sparks, faster material removal, but bigger craters and rougher finishes. Lower Ip means finer sparks, smoother cuts, but slower speeds. Here’s how I guide customers: for roughing passes (the first cut, where you’re removing most of the material), use a higher Ip—usually 8–12 amps for wire sizes 0.2–0.25mm. Roughing doesn’t need the smoothest finish, just speed to get close to the final dimension. Then, for finishing passes (the second or third cut, where you get the final surface quality and tolerance), drop Ip to 2–5 amps. Last month, a medical device shop was cutting stainless steel surgical guides, and their first pass left a Ra (surface roughness) of 3.2 µm, which was too rough for the part’s specs. Switching the finishing pass to 3 amps Ip brought their Ra down to 0.8 µm, exactly what the client required, without taking too much extra time. The only caveat: don’t run higher Ip than your wire size can handle. A 0.1mm wire maxes out at around 5 amps; run 10 amps through it, and it will snap immediately. Match Ip to your wire diameter, and you’ll avoid 90% of wire break issues.
Then there’s the Gap Voltage, or Servo Reference Voltage, which is often overlooked but critical for consistent spark generation. The gap voltage is the voltage between the wire and the workpiece; when it drops below a certain threshold, the machine knows there’s debris buildup or a short, and it slows the wire feed to give time for flushing. Most machines have a default gap voltage of 20–25 volts, but you can adjust this based on material. For conductive materials like aluminum or brass, which produce finer debris, a lower gap voltage (15–20 volts) works, because the smaller debris doesn’t need as much space to flush. For tough materials like hardened tool steel or titanium, which produce coarser, denser debris, bump gap voltage up to 25–30 volts. This widens the gap, giving the dielectric more room to work, reducing short circuits. I once had a mold shop cutting P20 tool steel, and their gap voltage was set to 20 volts, so they were getting constant shorts every time they hit a dense spot in the steel. Cranking to 28 volts eliminated the shorts, and their cut speed stayed steady throughout the 100mm cut, no stops.
Now, here’s the thing: these aren’t one-size-fits-all numbers. Every machine is a little different, every material is unique, and every part’s requirements (tolerance, surface finish, cut speed) change the parameters. That’s why I always tell customers to test parameters on scrap material first. Grab a few pieces of the same material you’ll be cutting, run small test cuts, and adjust Ton, Toff, Ip, and gap voltage incrementally—don’t make big jumps all at once. For example, if you’re cutting 20mm hardened D2 tool steel, start with Ton 22 µs, Toff 18 µs, Ip 7 amps, gap voltage 26 volts. Cut a 5mm x 5mm test section, measure the surface roughness, check for wire breaks, and adjust. If the finish is too rough, drop Ton by 2 µs and Ip by 1 amp. If there are wire breaks, add 3 µs to Toff and bump gap voltage by 2 volts.
I also can’t forget to mention the wire size, because that’s a huge variable most people miss. 0.25mm brass wire is thicker than 0.1mm molybdenum wire, so it can handle higher Ip, longer Ton, and shorter Toff. If you’re switching wire sizes, you have to adjust your parameters. Last quarter, a customer switched from 0.2mm to 0.15mm wire to cut smaller features, and they kept breaking wire because they used their old 0.2mm settings. Their Ip was 8 amps, which is way too much for the thinner 0.15mm wire—dropping to 4 amps fixed it instantly.
Another common mistake is ignoring the dielectric fluid’s condition, which ties into pulse parameters. If your deionized water has a conductivity that’s too high (over 10 µS/cm), the sparks become less focused, leading to rougher cuts and more wire breaks. Good dielectric conductivity is 2–6 µS/cm for most cuts, so if your machine’s reading is higher, replace or filter the fluid. Dirty dielectric means debris isn’t flushing, so even if your pulse parameters are perfect, you’ll get poor results. I always tell customers to check their dielectric conductivity weekly, because a dirty fluid messes with the pulse’s ability to create consistent sparks, no matter how much you adjust Ton or Toff.
At the end of the day, adjusting pulse parameters is all about balancing speed, finish, and wire longevity. You don’t want to go so fast that you snap wire, and you don’t want to take so long that you’re missing deadlines. As someone who’s supplied Wire Cut EDM equipment and training to hundreds of shops, I can tell you that the difference between a shop that’s constantly troubleshooting and one that’s running smoothly is usually just getting these parameters right. If you’re struggling with cuts that are too rough, wire breaks, or slow speeds, don’t guess at adjustments. Take the time to test on scrap, match parameters to material thickness and wire size, and don’t forget about the dielectric fluid.
If you’re ready to upgrade your Wire Cut EDM machine or need more tailored advice for your specific part runs, our team of EDM specialists is here to help. We work with shops of all sizes, from small job shops to aerospace manufacturers, to get their parameters dialed in and their machines running at peak efficiency. Reach out to us to discuss your needs, and we’ll walk you through the best settings for your materials, parts, and production goals.
Upgraded High Speed Wire EDM References:
- McGeough, J. A. (2002). Advanced Methods of Machining. Chapman and Hall.
- EDM Handbook: A Guide to Electrical Discharge Machining (2nd ed.). Society of Manufacturing Engineers.
- Webster, J. G. (Ed.). (1999). Instrumentation, Signals, and Sensors. CRC Press.
Taizhou Ouling CNC Equipment Co., Ltd.
As one of the most professional wire cut EDM manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy advanced wire cut EDM made in China here from our factory. Welcome to contact us for quotation.
Address: No. 9 jingang Road, Yangzhou City Jiangsu Province, China
E-mail: 574751243@qq.com
WebSite: https://www.oulingedm.com/
